Casting Sculptures with Epoxy Resin: An Advanced Next Step (Not a Starting Point)
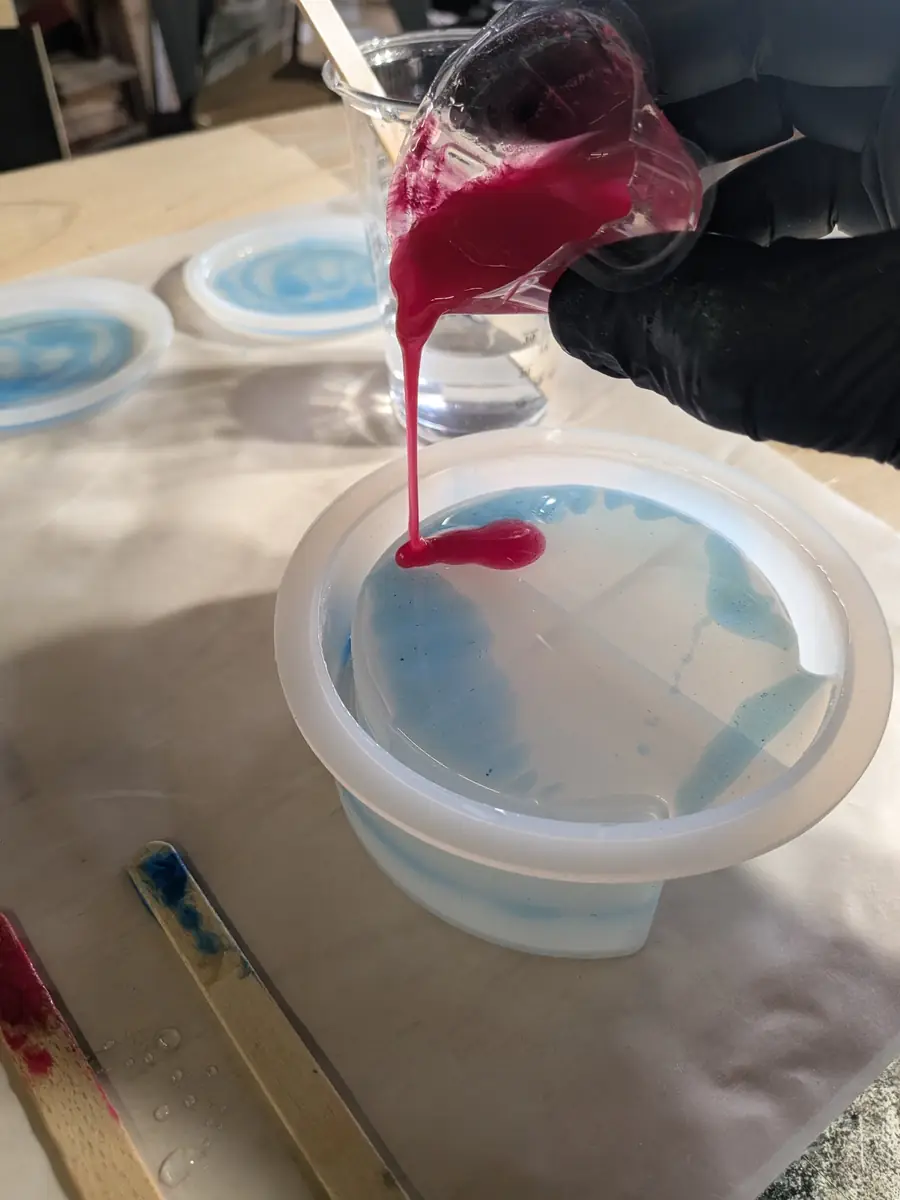
⚠️ New to resin? Start here instead. This guide assumes you’ve already mixed epoxy successfully at least once. If you’re just getting started, our Beginner Resin Guides hub and How to Mix Epoxy Resin are the right first stop — casting is genuinely one of the harder resin skills to learn first.
Key Takeaways
- Casting sculptures is a different discipline from coating a tray or board: you’re pouring resin into a mold, often in thick layers, which introduces heat and cure risks that flat pours don’t have.
- The single biggest risk at this stage is exotherm — the heat epoxy generates as it cures — which gets more dangerous the deeper and larger your pour. We’ll show you how to manage it safely.
- Everything in Resin PPE for Beginners still applies, plus a few casting-specific additions.
- Budget for failed attempts. Even experienced crafters lose pieces to cracking, yellowing, or trapped bubbles — that’s normal, not a sign you’re doing it wrong.
Table of Contents
- What “Casting” Actually Means
- Before You Start: Prerequisites
- Materials and Tools
- Understanding Exotherm (Read This Before You Pour)
- Step-by-Step: Casting a Small Sculpture
- Troubleshooting
- FAQ
- Where to Go From Here
1. What “Casting” Actually Means
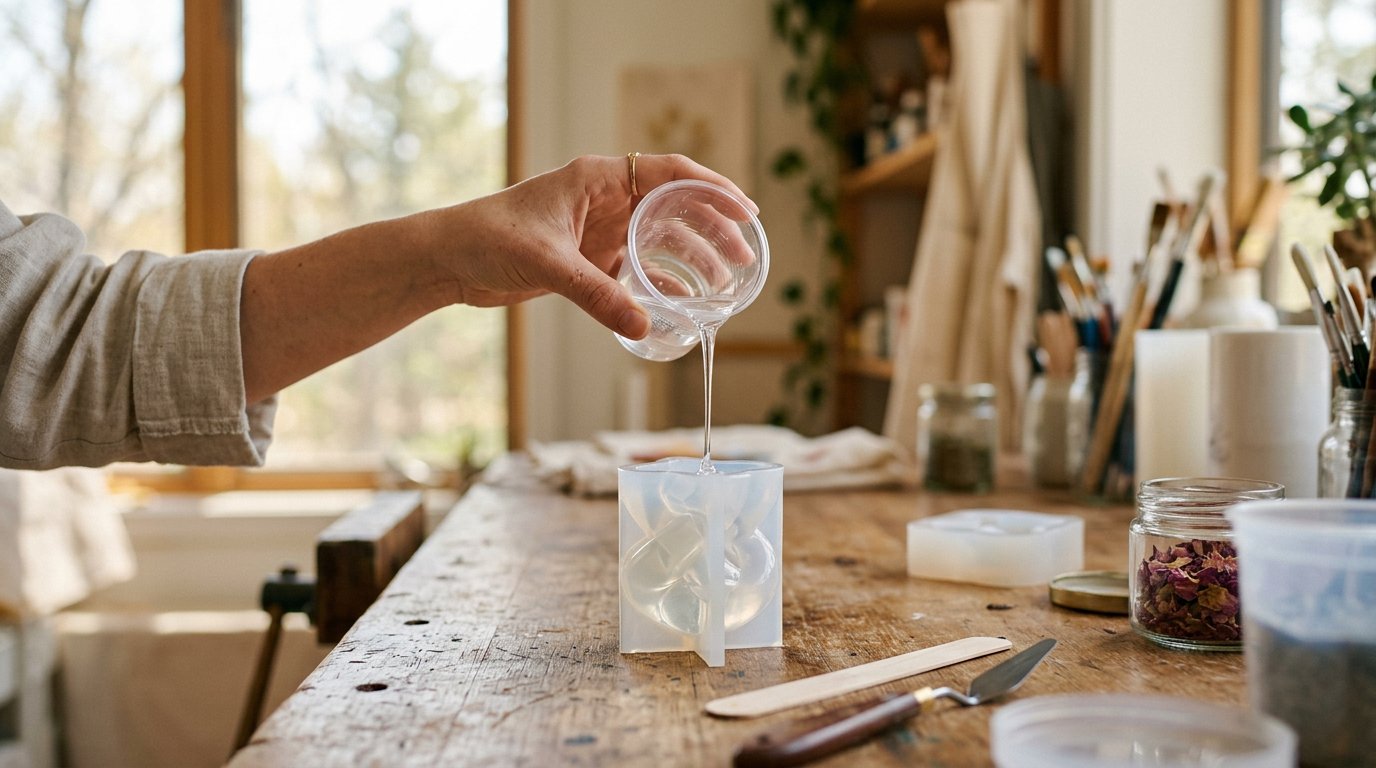
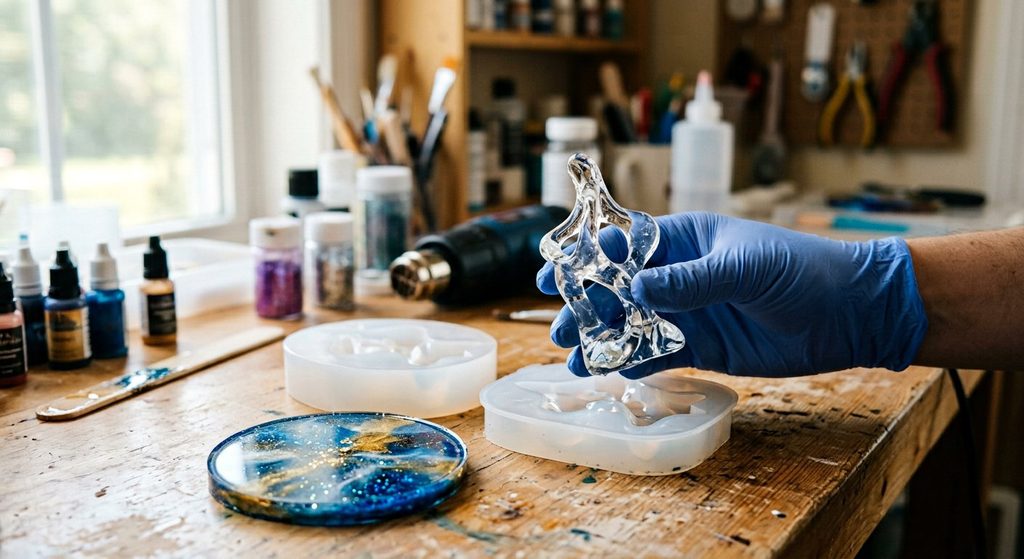
Coating a tray or topping a board is a flat pour — resin sits in a thin, wide layer with lots of surface area to release heat as it cures. Casting is different: you’re filling a three-dimensional silicone mold, often several inches deep, to produce a free-standing object once it’s demolded. Think small figurines, paperweights, jewelry blanks, or decorative sculptural pieces.
That extra depth is exactly what makes casting harder. A thin pour dissipates heat easily; a deep pour traps it, and resin’s curing reaction is exothermic — it generates its own heat as it hardens. Manage that heat well and you get a clear, crack-free piece. Get it wrong and you get cloudiness, cracking, yellowing, or in extreme cases enough heat to smoke, crack the piece, and burn whatever it’s sitting on. We cover exactly how to manage this in Section 4, and it’s worth reading before you buy any materials.
2. Before You Start: Prerequisites
This isn’t a gatekeeping exercise — it’s a genuinely practical checklist, because casting mistakes are more expensive (in time, materials, and sometimes safety) than a flat-pour mistake.
- ✅ You’ve successfully completed at least one flat-pour project (a coaster or serving tray) and are comfortable with accurate mixing ratios.
- ✅ You’ve read Is Epoxy Resin Safe? and have the PPE described in Resin PPE for Beginners on hand.
- ✅ You have a well-ventilated space you can dedicate to a multi-day cure without disturbance.
- ✅ You’re prepared for a slower process than a flat pour — thick casting resin has a longer working time and a slower cure than a coating resin; full cure runs from about 72 hours (Let’s Resin Deep Pour) to 5–10 days (TotalBoat ThickSet Fathom).
3. Materials and Tools
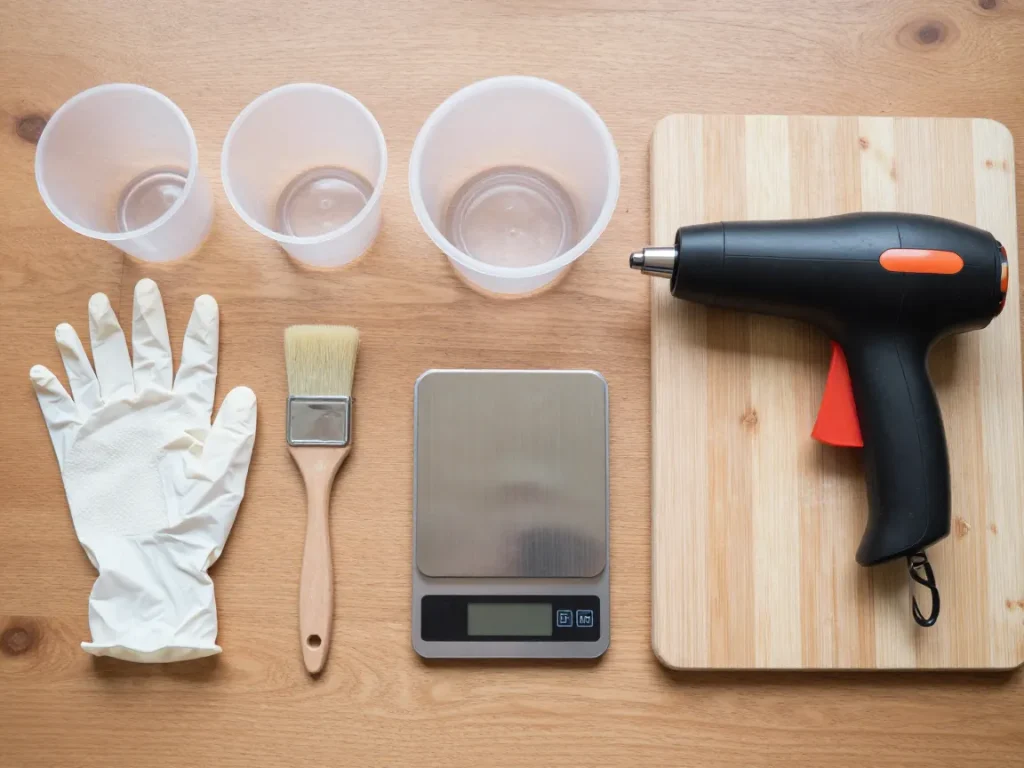
Start from the core kit in Essential Resin Tools Every Beginner Needs — gloves, respirator, goggles, graduated mixing cups, a digital scale, and stir sticks all still apply. Casting adds a few specifics:
| Item | Why You Need It | Beginner Tip |
|---|---|---|
| Deep-pour / casting-specific resin | Formulated to cure slower and cooler than standard art or table-top resin, specifically to manage exotherm | Never substitute a flat-pour resin for a deep casting — the heat buildup can be genuinely unsafe |
| Silicone molds (tin-cure or platinum-cure) | Flexible enough for clean demolding, and both types stand up to epoxy casting. Platinum-cure molds shrink least and last longest, so they’re worth it for a mold you’ll reuse | Start with a simple, single-cavity mold before attempting multi-part molds |
| Mold release spray (if your mold’s manufacturer recommends one) | Some molds need it, some don’t — check first | Test on a scrap edge if unsure |
| Graduated measuring cups (or a digital scale only if your label gives a by-weight ratio) | Measure the way your label says. Let’s Resin Deep Pour is 2:1 by volume, so use cups; TotalBoat gives both a volume and a weight figure, and they are different numbers because resin and hardener weigh different amounts | Never put a by-volume ratio on a scale, and don’t eyeball — even more true here than for a flat pour |
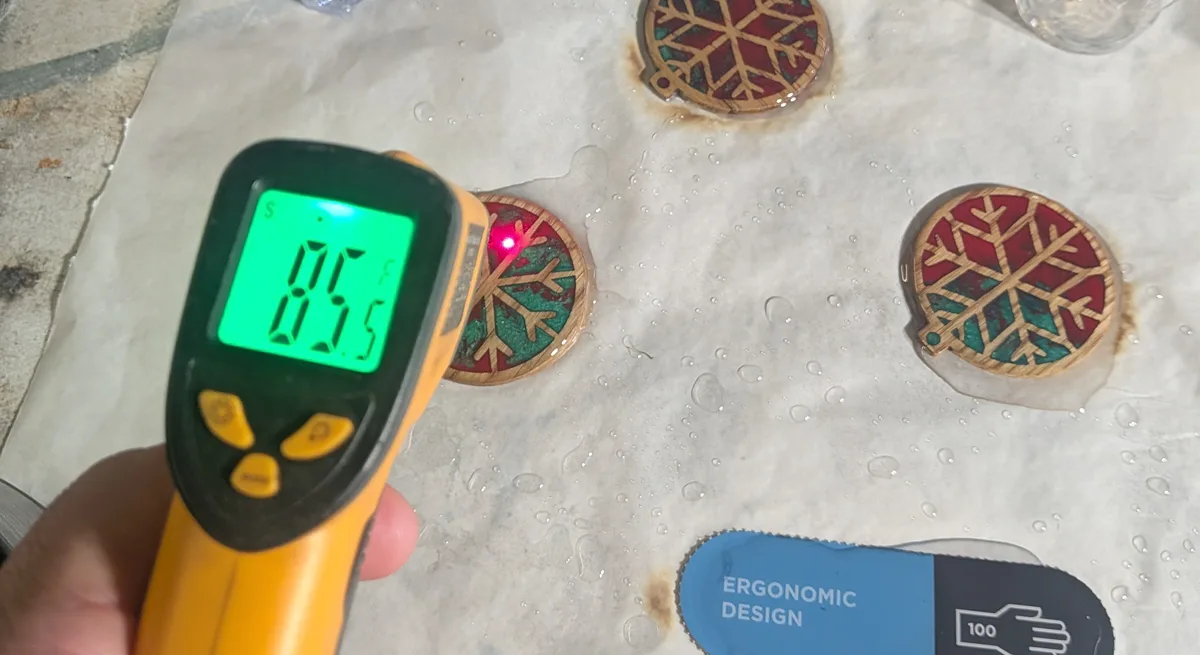
| Infrared or probe thermometer (optional but recommended) | Lets you watch the exotherm instead of guessing, and TotalBoat uses one to time the next layer (pour when the last layer is below 85°F) | Point-and-shoot IR thermometers are inexpensive and worth it for any layered pour |
| Heat-safe surface | A runaway pour can reach 200–400°F, enough to melt plastic or ignite what it’s sitting on, so pour on a surface that can take heat | A silicone mat on a wooden table is not a heat-safe surface for a large pour |
4. Understanding Exotherm (Read This Before You Pour)
This is the section that separates casting from every other resin project on this site, so we’re not going to bury it.
What’s happening: as epoxy cures, the chemical reaction between resin and hardener releases heat. In a thin, wide pour, that heat escapes into the air almost as fast as it’s generated. In a deep, contained pour, it can’t escape as easily — so the resin in the center of your mold gets hotter than the resin at the edges, and hotter than the room around it.
Why it matters:
- Too much heat can cause cracking right through the thickness of the piece, often starting in the center where the heat is trapped.
- It can cause a yellow or amber tint, shrinkage, or cracks that weren’t there in the liquid resin.
- In genuinely extreme cases — using the wrong resin for the pour depth, or pouring a single very large batch all at once — enough heat can build up to melt a plastic cup, scorch what the mold is sitting on, burn skin, and give off toxic fumes. This isn’t meant to alarm you; it’s meant to explain why every casting resin’s label is so specific about maximum pour depth, and why that number isn’t a suggestion.
How to manage it:
- ✅ Use a resin specifically rated for deep pours or casting — never a flat-pour formula.
- ✅ Respect the maximum single-pour depth on your product’s label. If you want a taller piece, most casting resins are designed to be poured in layers over multiple days rather than all at once — check your product’s guidance on layering. For example: Let’s Resin Deep Pour allows 2–4 in per pour; TotalBoat ThickSet 2 in for castings under 10 fl oz; TotalBoat ThickSet Fathom 3 in for castings under a gallon; Alumilite Amazing Deep Pour 2 in. Between layers, TotalBoat ThickSet says at least 4 hours; ThickSet Fathom says at least 36 hours, or 24 hours if an infrared thermometer shows the last layer is below 85°F. Let’s Resin gives no layering interval, so wait until the first layer is cool and firm.
- ✅ Pour in a room held steady at 70–80°F (21–27°C), and check your label: Let’s Resin Deep Pour says 75–85°F, TotalBoat ThickSet 65–75°F and TotalBoat ThickSet Fathom 60–80°F, with 70°F best for thick pours. Hotter rooms speed the reaction and raise the exotherm; colder rooms slow or stall the cure.
- ✅ If you have a thermometer, it’s normal to see the center of a curing piece run noticeably warmer than the room. A sudden spike in heat, smoke, or a strong chemical smell beyond your resin’s normal cure odor means the cure is running away. Don’t pick it up: a runaway mass can reach 200–400°F and will burn skin, and the fumes are toxic (an organic-vapor respirator may not stop them). Leave it where it is, open windows, point a fan to push the vapors away from you, keep people and pets out, and let it finish. Set every pour up on a heat-safe surface in the first place so you never have to move a hot one.
- ✅ Larger molds generally need more caution than small ones — this is a good reason to start with a small piece, not a large one, for your first cast.
5. Step-by-Step: Casting a Small Sculpture
Step 1: Choose a Simple First Mold
Pick a small, single-cavity silicone mold — something in the 1–3 inch range, like a paperweight or small figurine mold — for your first attempt. Save multi-part or large molds for after your first successful cast.
Step 2: Prep Your Workspace
Set up on a level, heat-safe surface in a well-ventilated room, with your PPE on before you open any bottles. Lay down a silicone mat to catch drips.
Step 3: Prep the Mold
If your mold’s manufacturer recommends a release agent, apply a thin, even coat now and let it fully dry per their instructions. Check the mold is clean, dry, and free of dust or lint, which will be permanently visible in a clear cast.
Step 4: Measure and Mix
Measure your resin and hardener exactly as your label says: by volume in graduated cups for Let’s Resin Deep Pour (2:1 by volume), or by weight on a scale only if your label gives a by-weight figure. Stir slowly for at least 3 minutes, scraping the sides and bottom of the cup, then pour the mix into a second clean cup and stir for 1–2 minutes more. Slow stirring keeps air out.
Step 5: Pour in Stages
For anything deeper than your resin’s single-pour rating, pour in layers rather than all at once — check your product’s specific layering guidance for how long to wait between pours. For a small first piece within the single-pour limit, pour slowly in one steady stream to help air escape as you go.
Step 6: Address Bubbles Carefully
A heat gun is fine for surface bubbles on a deep pour: Let’s Resin and TotalBoat both recommend it. Keep it moving about 6–8 inches above the surface, a few seconds at a time, and don’t singe the resin. Use a heat gun, not a torch, on a silicone mold. A toothpick works for the odd stubborn bubble.
Step 7: Let It Cure — Fully
Resist the urge to check on it. Deep-pour resins are formulated to cure slowly on purpose; disturbing or moving the mold early is one of the most common causes of cracking. Follow your product’s full cure schedule, which runs from about three days to more than a week depending on the resin.
Step 8: Demold
Once fully cured, gently flex the silicone mold away from the piece rather than pulling the piece straight out. If it resists, don’t force it — let it cure another day and try again.
Step 9: Finish
Sand any mold seam lines starting at a low grit and working up, then polish. Cured casting resin can be sanded and polished: TotalBoat says to wait 5–7 days before wet sanding or buffing, and Let’s Resin suggests sanding and polishing for a satin finish, or a top coat of table-top epoxy for high gloss.
6. Troubleshooting
| Problem | Likely Cause | Fix |
|---|---|---|
| Cracking, especially in the center | Exotherm — pour was too deep or too large for the resin’s rating | Use a properly rated deep-pour resin and respect max layer depth; pour in stages |
| Cloudy or milky finish | Cold resin, under-mixing, whipping air in, or moisture and high humidity | Re-check your mixing technique, warm the resin to room temperature, mix slowly for the full time, keep tools and inclusions dry, and keep humidity at 60% or lower |
| Piece won’t release from the mold | Missing or uneven release agent, or incomplete cure | Confirm full cure time has passed; check your mold manufacturer’s release recommendations |
| Trapped bubbles inside the piece (not just surface) | Air introduced during mixing or pouring too fast | Mix more slowly; pour in a thin, steady stream rather than dumping |
| Yellow tint appearing over time | UV exposure or excess heat during cure | Choose a UV-stable formula and keep curing pieces out of direct sunlight |
7. FAQ
Can I use the same resin I used for my coasters or tray?
Not for anything beyond a shallow mold. Standard art or table-top resin isn’t formulated to manage exotherm at depth — check your product’s maximum pour thickness before assuming it’ll work.
Do I need a pressure pot or vacuum chamber for casting?
Not for the small first pieces in this guide. Those tools reduce bubbles further and are common among more advanced casters, but per our essential tools guide, they’re not something to buy before you’ve mastered the basics.
How long does a cast piece actually take to cure?
It depends on the resin and the pour. Let’s Resin Deep Pour demolds in 8–12 hours and fully cures in 48–72 hours; TotalBoat ThickSet demolds after 24 hours and fully cures in 3–5 days; TotalBoat ThickSet Fathom demolds after 48–72 hours and fully cures in 5–10 days. Follow your label, and don’t demold while the piece feels soft or rubbery.
Is it normal for my mold to feel warm while curing?
Mild warmth is expected — that’s the exotherm reaction discussed above. A sudden spike in heat, smoke, or a strong unusual smell is not normal; don’t pick it up (a runaway mass can burn skin and gives off toxic fumes); open windows, use a fan to push the vapors away, keep people and pets out, and let it finish where it sits.
My piece cracked. Did I do something wrong?
Probably, but don’t be discouraged — cracking from exotherm is one of the most common casting mistakes even among experienced hobbyists, and it’s almost always fixable by pouring shallower, in more stages, or switching to a resin properly rated for your pour depth.
8. Where to Go From Here
If this guide felt like a lot, that’s by design — casting is genuinely one of the more advanced resin skills, and there’s no shame in going back to build more confidence with flat pours first. The Beginner Resin Guides hub is the best place to do that, and the Resin Safety Hub is worth bookmarking as you take on projects with more materials and more risk. If you’re specifically interested in bigger flat-pour projects before tackling casting, our guide to epoxy butcher block is a good middle step.
Sources
- Let’s Resin: Deep Pour Resin instructions (PDF): 2:1 by volume, stir at least 3 minutes, 60–80 minute working time, 2–4 in per pour, demold 8–12 hours, full cure 48–72 hours, 75–85°F, heat gun for surface bubbles
- Let’s Resin: Deep Pour Epoxy Resin: 2–4 in single-layer pours and an 80-minute working time
- TotalBoat: ThickSet Epoxy instruction sheet and TDS: 1:1 by volume or 1.11:1 by weight, 2 in max for small castings, 65–75°F, demold 24 hours, full cure 3–5 days, heat gun 6–8 in above the surface, 4 hours between layers, 5–7 days before wet sanding
- TotalBoat: ThickSet Fathom technical data sheet (PDF): 2:1 by volume or 100:43 by weight, 3 in max for small molds, 60–80°F with 70°F best for thick pours, demold 48–72 hours, full cure 5–10 days, a few seconds of heat gun at a time, 200–300°F if poured too thick, don’t demold while soft
- Alumilite: Amazing Deep Pour: 2 in per layer, up to 60 minutes working time, 5–7 days full cure, low-exotherm formula
- WEST SYSTEM: The basics of uncontrolled cure: a 100-gram mass can reach 400°F; a runaway cure can melt plastic, burn skin and ignite combustibles; the vapors are toxic and an air-purifying respirator may not stop them; set the container where you can watch it and use a fan
- Epoxyworks (WEST SYSTEM): Controlling exotherm: heat builds when it can’t escape, thin films stay cool, runaway epoxy can foam, smoke and give off dangerous vapors, and high temperature cracks cured epoxy
- Smooth-On: What is silicone rubber?: tin-cure silicone stands up to epoxy casting; platinum-cure shrinks least and lasts longest
- Smooth-On: Do I measure by weight or by volume?: by-weight and by-volume ratios are different numbers because the two parts have different densities; confirm which one your label gives
- ArtResin: Why is my resin cloudy?: cold resin, under-mixing, whipping air in, moisture and high humidity cause cloudiness
- ArtResin: Why does my resin look yellow?: UV light is the most common cause of yellowing; sustained heat also discolors resin
- ArtResin: Tips to prevent resin bubbles: stir slowly and scrape, pour slowly and steadily, a heat gun rather than a torch on silicone molds, 1/8 in max per layer for a coating resin
Keep Learning on ResinAffairs.com
More guides to read next:
- 🧩 Best Resin Molds for Beginners → — silicone vs. plastic vs. DIY molds, and which one to buy for each project.
- 💍 Resin Jewelry for Beginners → — pendants, earrings and charms, the easiest way to start with UV resin.
- 🌊 Epoxy River Table for Beginners → — put your deep-pour and heat-control skills to work on a small wood-and-resin river table.
- 🩹 Common Resin Problems and How to Fix Them → — fixes for stickiness, bubbles, soft spots and cracks on any resin project.
Alex is not a chemist or safety engineer; always follow your specific resin manufacturer’s data sheet and safety guidance, and consult a qualified professional for any health or ventilation concerns specific to your workspace.
Enjoyed this guide? Join the Resin Affairs newsletter for new tutorials, safety tips, and project ideas straight to your inbox.